Casting vs Forging: How to Choose the Right Manufacturing Process
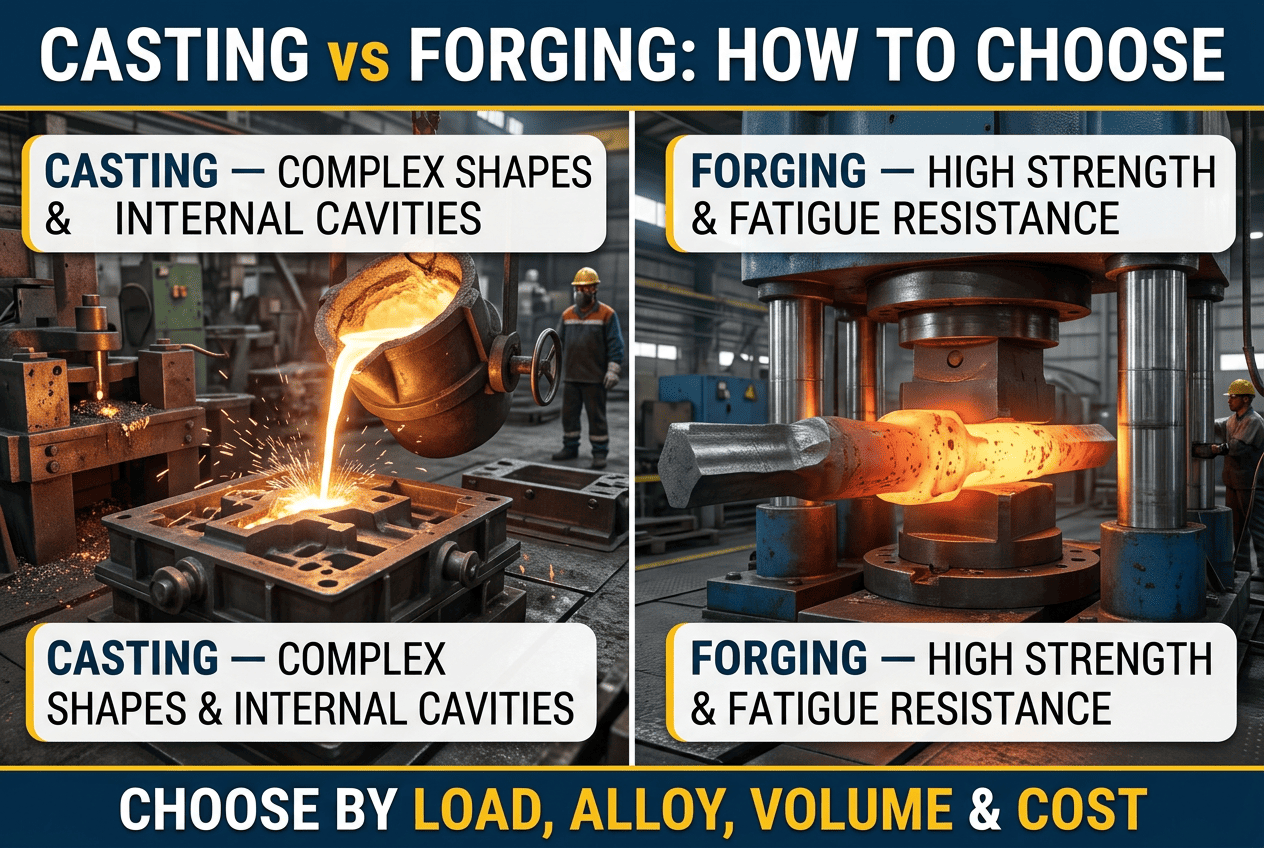
Direct Answer:Casting pours molten metal into a mould, so it suits complex shapes, internal cavities, large parts and a wide range of alloys at lower tooling cost. Forging shapes solid metal under compressive force, which refines grain structure and generally gives higher strength, toughness and fatigue resistance for load-bearing parts. Choose by working through six questions: what loads and failure risks the part faces, how complex the geometry is, which alloy you need, what volume you expect, what tooling budget and lead time you have, and which inspection standards apply. Then qualify the supplier, not just the process, and lock quality, ownership of tooling, Incoterms, warranty and exit terms into the contract. GTsetu helps manufacturers find government‑tie‑up verified suppliers and partners across 100+ countries, with anonymous discovery, built-in NDA workflows and zero broker commission.
📅 Published October 14, 2026🔄 Updated October 14, 2026⏱ 15 min read✍️ GTsetu Editorial Team
2
Core Processes Compared
10
Decision Factors
100+
Countries on GTsetu
0%
Broker Commission
Choosing between casting and forging looks like an engineering question, and it is. But it is also a sourcing, cost and risk question. The wrong process can mean a part that cracks in service, a tooling bill that never pays back, or a supplier who cannot deliver the quality you specified. Getting it right early saves redesign, scrap and warranty claims later.
Procurement leads, design engineers, product managers and founders who need to specify, compare or source metal components, and exporters or importers deciding which supplier capability to look for in a new market.
⚖️ Engineering & Legal Disclaimer
This guide provides general commercial and educational information and does not constitute engineering, legal, tax or regulatory advice. Material properties, process capability and standards vary by alloy, supplier and application. Validate critical parts with qualified engineers, standards and testing, and obtain legal advice before signing supply agreements.
SECTION 1
1 What Is the Difference Between Casting and Forging?
🎯 Definition
Casting is a process in which molten metal is poured into a mould cavity and allowed to solidify into the desired shape. Forging is a process in which solid metal, usually heated, is shaped by compressive force from hammers or presses. Casting builds the shape by filling a cavity; forging builds it by deforming metal that is already solid.
That one difference drives almost everything else. Because cast metal solidifies from a liquid, it can fill intricate cavities, but it can also trap gas, shrink unevenly and develop a less uniform internal structure. Because forged metal is deformed while solid, its internal grain is worked and aligned with the shape of the part, which generally improves strength and fatigue behaviour, but limits how complex the geometry can be.
Why the Choice Matters
🔩
Performance in Service
Load, impact and fatigue requirements decide whether a part can safely use the process you prefer.
💰
Total Cost
Tooling, material yield, machining, scrap, inspection and freight all change with the process, not just the part price.
⏱️
Speed to Market
Tooling lead times and first-article approval can add weeks or months. Plan around the slowest step.
🛡️
Supply Risk
Few suppliers excel at both processes. Your choice narrows the field of qualified partners you can use.
“Casting” and “forging” are families of processes, not single methods. Comparing a sand casting with a closed-die forging is a very different decision from comparing investment casting with open-die forging, so identify the specific process you are considering.
Common Casting Methods
Sand
Sand Casting
Metal is poured into expendable sand moulds. Flexible for large parts and low volumes; rougher surface and looser tolerances.
Large & flexible
Investment
Investment Casting
A wax pattern is coated in ceramic, melted out, then filled with metal. Fine detail and good surface finish; higher cost per part.
Fine detail
Die
Die Casting
Molten metal is forced into reusable steel dies under pressure. Fast and repeatable for high volumes, mainly in non-ferrous alloys.
High volume
Centrifugal
Centrifugal Casting
A spinning mould pushes metal outward as it solidifies. Suited to pipes, rings and sleeves with dense walls.
Tubular parts
Common Forging Methods
Open-Die
Open-Die Forging
Metal is shaped between flat or simple dies. Suited to very large or one-off parts and short lead times on tooling.
Large & custom
Closed-Die
Closed-Die (Impression) Forging
Metal is pressed into shaped dies. Repeatable and strong for medium to high volumes; die cost is significant.
Repeatable
Ring-Rolled
Seamless Ring Rolling
A pierced preform is rolled into a seamless ring. Common for bearings, flanges and turbine components.
Seamless rings
Cold
Cold & Warm Forging
Forming at lower temperatures gives good surface finish and tight tolerances on smaller parts, with higher forming forces.
Precision small parts
✨ GTsetu Insight
Ask suppliers which exact process variant they would use and why. A foundry that only does sand casting and a forge that only does open-die work will each tend to recommend what they can make. Independent engineering input, or a trusted consultant (see international business development consulting), helps you avoid a supplier-driven choice.
SECTION 3
3 Casting vs Forging: Head-to-Head Comparison
The table below summarises typical tendencies. Real results depend on the specific alloy, process variant, supplier capability and inspection regime, so treat it as a starting point for discussion with engineers, not a specification.
Factor
Casting
Forging
Strength & Toughness
Good, but generally lower and less uniform than forged
Generally higher, with strong impact and fatigue resistance
Internal Structure
Random grain; risk of porosity, shrinkage and inclusions
More limited: simpler shapes, often finished by machining
Part Size
Very small to very large, depending on method
Small to very large, with open-die suited to the largest
Material Range
Very wide, including alloys that are hard to forge
Wide, but some alloys are difficult to deform
Surface Finish & Tolerance
Varies from rough (sand) to fine (investment, die)
Good, especially cold forging; often machined to final size
Tooling Cost
Often lower, especially for sand and low volumes
Often higher for closed dies; open-die tooling is simple
Best Volume Range
Prototype to very high (die casting)
Medium to high for closed-die; custom for open-die
Lead Time
Short for sand; longer for complex investment tooling
Die manufacture can be slow; open-die can be quick
Typical Failure Concern
Hidden porosity and shrinkage defects
Laps, folds and incomplete fill if poorly controlled
SECTION 4
4 Strength, Grain Structure & Typical Defects
Strength is the most common reason to choose forging, and the reason is structural. Forging compresses and works the metal, closing internal voids and aligning grain flow along the contours of the part, so stress is carried along the grain rather than across it. Cast metal solidifies without that working, so its grain is more random and defects are more likely to hide inside.
✅ Where Casting Wins
✅Complex geometry: internal passages, undercuts and thin walls that cannot be forged.
✅Near-net shape: less machining and less wasted material on intricate parts.
✅Alloy flexibility: alloys that are brittle or hard to deform can often still be cast.
✅Lower entry cost: simpler tooling suits prototypes and small runs.
✅Scale: very large and very small parts are both feasible depending on method.
⚠️ Where Casting Needs Care
⚠️Porosity and shrinkage: gas pockets and voids can reduce strength and cause leaks.
⚠️Inclusions: trapped slag or oxides can act as crack starters.
⚠️Lower fatigue life: a risk under cyclic or impact loading without strict control.
⚠️Process variability: results depend heavily on foundry discipline and inspection.
⚠️Hidden defects: some flaws are only visible with non-destructive testing.
✅ Where Forging Wins
✅Strength and toughness: refined grain flow handles high loads and impact.
✅Fatigue resistance: well suited to rotating and cyclically loaded parts.
✅Structural integrity: fewer internal voids and more consistent properties.
✅Reliability: preferred where failure would be costly or dangerous.
✅Repeatability at volume: closed-die forging gives consistent parts once dies are proven.
⚠️ Where Forging Needs Care
⚠️Shape limits: intricate internal features usually require machining after forging.
⚠️Die cost: closed-die tooling is a major upfront investment.
⚠️Laps and folds: poor die design or process control can create surface defects.
⚠️Lead time: die design and proving can take time before the first good part.
⚠️Machining allowance: some designs need extra stock to be machined away.
SECTION 5
5 Cost, Volume & Lead Time
The cheapest process on a quote is not always the cheapest process in service. Compare total landed and lifecycle cost: tooling, material yield, machining, heat treatment, inspection, scrap, freight, duties and the cost of failure.
Cost Driver
What to Ask
Practical Tip
Tooling
Pattern, die or mould cost, expected tool life, who owns it
Spread tooling over realistic volumes and agree ownership in writing.
Material Yield
How much metal ends up in the finished part versus scrap or machining
Near-net shapes can save material on complex parts; simple shapes may favour forging.
Machining & Finishing
Stock allowance, tolerances, heat treatment and surface requirements
Quote the finished part, not the raw casting or forging.
Quality & Scrap
Expected rejection rate, inspection scope and rework
Define who pays for rejected parts and hidden defects found later.
Volume & Run Length
Annual quantity, batch sizes and ramp-up plan
Low volumes often favour casting or open-die; high volumes can justify closed-die tooling.
Freight & Duties
Weight, packaging, transit time and import duties
Heavy parts make freight a major part of landed cost. Model it early.
✨ GTsetu Insight
A useful test: calculate cost per installed, accepted part, including expected scrap and one realistic failure scenario. A process that looks 15% dearer per piece can win once rework and warranty exposure are included.
SECTION 6
6 Decision Guide: Which Process Fits Your Part?
Work through these questions in order. If several answers point to different processes, the part may need a design change, a hybrid approach (for example a forged blank with machined features) or an engineer’s review.
🧭 Quick Selection Guide
Heavy load, impact or cyclic stress?
Yes, failure is costly
Lean Forging
Fatigue life and reliability usually favour forged, grain-aligned parts.
Complex internal cavities or thin walls?
Yes
Lean Casting
Cavities and intricate geometry are hard or impossible to forge.
Alloy hard to deform?
Yes
Lean Casting
Some alloys are practical to cast but difficult to forge.
Prototype or low volume, limited tooling budget?
Yes
Lean Casting / Open-Die
Simpler tooling reduces upfront cost and speeds the first part.
Medium to high volume, simple shape, demanding use?
Yes
Lean Closed-Die Forging
Die cost spreads over volume and parts stay consistent.
Very high volume, small non-ferrous parts?
Yes
Consider Die Casting
Fast cycle times and repeatability suit mass production.
📌 Hybrid and Alternative Routes
You are not always choosing one or the other. Many designs use a forged or cast blank that is then machined, heat treated or welded. Fabrication, powder metallurgy and machining from bar are also worth a look when the shape and volume suit them. Ask suppliers for an alternative route if your first choice looks costly.
SECTION 7
7 Applications by Industry
Industry practice is a helpful reality check, but it is not a rule. Always verify the process against the specific load case, standard and customer requirement for your part.
Sector
Typically Cast
Typically Forged
Automotive
Engine blocks, cylinder heads, housings, wheels
Crankshafts, connecting rods, gears, axle and steering parts
Aerospace
Turbine blades and complex housings (often investment cast)
Landing gear, structural fittings, discs and shafts
Oil, Gas & Energy
Valve bodies, pump casings, impellers
Flanges, pressure-containing parts, shafts and rings
Industrial Machinery
Gearbox housings, machine bases, pump components
Gears, shafts, couplings and heavy-duty fasteners
Construction & Mining
Large housings, counterweights, wear parts
Hooks, pins, links and load-bearing components
Medical & Hospitality
Implant components and equipment parts, depending on alloy
Surgical tools and high-strength fittings
✨ GTsetu Insight
Engineering ecosystems shape where capable suppliers cluster, and where design talent for advanced components sits. For an example of a regional cluster worth watching, see how Maharashtra’s FTI is shaping quantum technology in Pune.
SECTION 8
8 Quality, Testing & Certifications
For cast and forged parts, quality is mostly invisible at delivery: the defects that matter sit inside the metal. Specify what must be tested, to which standard, and who pays, before you place an order.
Check 01
Material Certification
Request mill or foundry test certificates that trace each batch to its chemistry and mechanical properties.
Check 02
Non-Destructive Testing
Agree methods such as ultrasonic, radiographic, magnetic-particle or dye-penetrant testing, and acceptance levels.
Check 03
Mechanical & Metallurgical Tests
Tensile, impact, hardness and microstructure tests confirm properties against your specification.
Check 04
Heat Treatment Records
Confirm cycles, furnace calibration and records, since heat treatment strongly affects final properties.
Check 05
Dimensional Inspection
Agree first-article inspection, sampling plans and gauges, and check the supplier’s measurement capability.
Check 06
Traceability
Require heat or lot numbers on parts and documents so any problem can be traced back to its batch.
A capable process on paper is only useful if the supplier executes it consistently. Many foundries and forges look similar in brochures; the differences show up in inspection records, scrap rates and how they behave when something goes wrong.
1
Define the Part and Process Requirements
Freeze drawings, material specification, tolerances, test requirements, volumes and delivery plan so every supplier quotes the same thing.
2
Build a Longlist from Several Channels
Use industry associations, trade fairs, buyer referrals, export promotion bodies and verified platforms. Our guide to international wholesale distributors helps if you also need a stocking or reselling partner.
3
Score Against Clear Criteria
Rate process capability, capacity, quality system, financial standing, compliance and cultural fit. Use our partnership evaluation criteria as a template.
4
Verify and Audit
Verify registration and ownership, check certificates with issuers, audit the plant or hire a third-party auditor, and inspect sample parts. See commercial due diligence for a structured approach.
5
Pilot Before You Scale
Start with first-article approval and a small production lot, then increase volume as quality and delivery performance are proven. Keep a qualified second source for critical parts.
Put the supply relationship into a written agreement. For cast and forged components, a few clauses carry most of the risk: specification and acceptance, tooling ownership, price and delivery terms, warranty, and how the relationship can end.
Topic
What to Define
Practical Tip
Specification & Acceptance
Drawings, material grade, tests, acceptance criteria, inspection rights
Attach the specification to the contract and state how disputed results are resolved.
Tooling Ownership
Who owns patterns and dies, who maintains them, and what happens at termination
Agree that you can retrieve your tooling and drawings if the relationship ends.
Price & Payment
Price basis, currency, payment timing, security and raw-material price adjustments
For new suppliers, consider staged payments, letters of credit or inspection before release.
Incoterms
Who arranges transport, insurance and clearance, and where risk transfers
Decide who bears the cost of defects found after machining or assembly before the first order, not after. For a wider framework on allocating these risks, see risk allocation in cross-border deals.
SECTION 11
11 Red Flags to Recognise Early
None of these signs is automatically fatal, but each deserves a direct answer before you commit tooling money or place volume orders.
🚩
Process Chosen by the Supplier’s Convenience
A recommendation that matches only what the supplier happens to make, without a technical reason tied to your load case.
🚩
No Test Reports or Traceability
Reluctance to share material certificates, NDT results or lot traceability for structural parts.
🚩
Unverifiable Certificates
Certificates that cannot be confirmed with the issuing body, or that do not match the entity you would contract with.
🚩
Opaque Ownership or Subcontracting
Unclear legal entity, or work quietly subcontracted to plants you have never audited.
🚩
Quote Far Below Competitors
A price that looks too good may reflect weaker material, skipped inspection or hidden extras later.
🚩
Resistance to Audits or Samples
Unwillingness to allow plant visits, third-party audits or first-article approval before volume production.
✨ GTsetu Insight
Identity gaps and weak early diligence sit behind many failed supplier relationships. See our guide on why trust breaks in global deals for the failure patterns to avoid.
SECTION 12
12 The Final Pre-Order Checklist
Use this list before you commit tooling or place a volume order. If you cannot tick an item, resolve it first.
Area
Confirm Before Ordering
Load Case
Loads, impact, fatigue and environment defined; failure consequences understood.
Process Choice
Specific casting or forging method chosen on geometry, alloy, volume and budget; alternatives considered.
Specification
Drawings, material grade, tolerances, tests and acceptance criteria frozen and attached to the contract.
Supplier Identity
Legal names, registered addresses and registration numbers checked against official records; ownership understood.
Capability Evidence
Certificates verified with issuers, plant audited, samples inspected and references contacted.
Tooling
Cost, lead time, tool life, ownership and retrieval rights agreed in writing.
Money
Total landed cost modelled; price, currency, payment security, Incoterms and taxes documented.
Quality & Warranty
Inspection scope, traceability, defect handling, warranty and liability terms agreed.
Supply Resilience
Second source or contingency plan identified for critical parts.
Exit & Disputes
Termination grounds, notice, stock and tooling return, governing law and forum chosen with legal advice.
PLATFORM
13 How GTsetu Helps Manufacturers Find Suppliers
🌐 Platform Spotlight, GTsetu
Your Verified Gateway to Suppliers & Partners
The hardest part of sourcing cast and forged components is often the first step: finding a supplier who actually exists as described, and sharing drawings safely. GTsetu connects manufacturers with government‑tie‑up verified suppliers and partners across 100+ countries, with built-in NDA workflows and encrypted collaboration. Every company on GTsetu is verified through direct government tie‑ups across six credentials: legal name, registered address, registration number, company status, company type, and date of certificate of incorporation. GTsetu does not verify industry certifications, financial standing, production capability or references; those must be checked directly between partners during due diligence.
✅
Government Tie‑Up Verification
6‑point verification: legal name, registered address, registration number, company status, company type, incorporation date.
📜
Certifications & Financials
GTsetu does not verify these. Exchange and validate them directly between partners.
🕵️
Anonymous Discovery
Explore supplier profiles without revealing your identity until mutual interest is confirmed.
📄
Built-In NDA Workflow
Formalise confidentiality before sharing drawings, pricing or strategy, with a full digital audit trail.
🚫
Zero Commission
No broker fees on any deal, whether a supply contract, distribution agreement or technology partnership.
🔐
Encrypted Collaboration
Documents and communications encrypted in transit and at rest. Secure B2B collaboration from first contact.
🌍
100+ Countries
A verified network of distributors, importers and supply chain partners.
QWhat is the difference between casting and forging?
Casting pours molten metal into a mould and lets it solidify, which suits complex shapes and a wide range of alloys. Forging shapes solid metal under compressive force, usually with heat, which refines the grain structure and generally gives higher strength, toughness and fatigue resistance. The better choice depends on geometry, performance requirements, volume and budget.
QIs forging stronger than casting?
In general, yes. Forging aligns the metal’s grain flow with the part’s shape and reduces internal voids, which typically improves strength, toughness and fatigue life compared with an equivalent cast part. Modern casting with good process control can meet many structural requirements, so compare the specific alloy, process and inspection requirements rather than relying on a rule of thumb.
QWhich is cheaper, casting or forging?
Casting is often cheaper for complex shapes and low to medium volumes because tooling can be simpler and less material is wasted in machining. Forging tooling is usually costlier, but unit cost can fall at higher volumes and the parts may need less rework in demanding applications. Compare total cost, including machining, scrap, inspection, freight and failure risk, not only the part price.
QWhen should I choose casting over forging?
Choose casting when the part has complex internal passages or intricate geometry, is very large, uses an alloy that is hard to forge, or when tooling budget and early-stage flexibility matter more than peak mechanical performance. Specify inspection and acceptance criteria clearly for safety-critical cast components.
QWhen should I choose forging over casting?
Choose forging when the part carries high loads, impact or cyclic stress, when fatigue life and reliability are critical, or when the geometry is relatively simple and volumes justify the tooling. Typical examples include shafts, crankshafts, connecting rods, gears, flanges and structural components.
QHow do I qualify an overseas casting or forging supplier?
Verify company identity and registration, review quality certifications with the issuer, audit the plant or arrange a third-party audit, inspect sample parts and test reports, check capacity and tooling ownership, and contact references. Match the depth of due diligence to the part’s criticality and your financial exposure.
QHow does GTsetu help with finding casting and forging suppliers?
GTsetu helps manufacturers find and verify suppliers and partners across 100+ countries. Every company is verified through government tie-ups on six core credentials (legal name, registered address, registration number, company status, company type, incorporation date). GTsetu offers anonymous discovery, built-in NDA workflows, encrypted collaboration and zero broker commission. GTsetu does not verify certifications, financial standing or production capability, so those must be checked directly between partners.
Ready to Find a Verified Casting or Forging Supplier?
Join 500+ verified manufacturers, exporters and distributors already building cross-border partnerships on GTsetu, with government‑tie‑up verification of six core credentials, built-in NDA workflows and zero broker fees across 100+ countries.
They represents the product, and research team behind GTsetu, a global B2B collaboration platform built to help companies explore cross-border partnerships with clarity and trust. The team focuses on simplifying early-stage international business discovery by combining structured company profiles, verification-led access, and controlled collaboration workflows.
With a strong emphasis on trust, and disciplined engagement, Team GTsetu shares insights on global trade, partnerships, and cross-border collaboration, helping businesses make informed decisions before entering deeper commercial discussions.